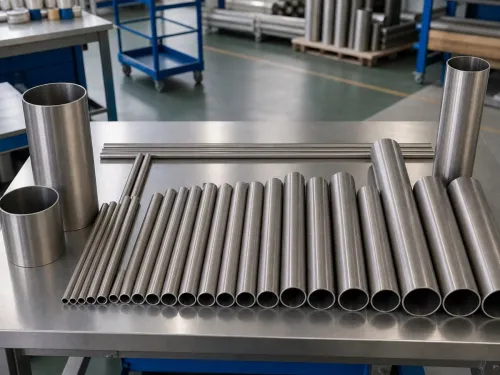
Titanium Exhaust Tubing & Laser-Cut Pie Cuts (Grade 1 & Grade 2)
Thin-Wall Titanium Exhaust Tubing & Weld-Ready Pie Cuts
Building a titanium motorsport exhaust system requires tubing that forms cleanly without splitting, welds with a calm puddle, and survives high-frequency thermal cycling without cracking. Through our certified partner facilities, we supply thin-wall commercially pure titanium exhaust tubing and rotary-laser-cut pie cuts engineered specifically for Motorsport & Exhaust Fabrication.
Why CP Grade 1 / Grade 2 and 1.0–1.2 mm (0.039”–0.047”) Wall?
For custom headers, downpipes, and cat-back systems, alloy selection and wall thickness dictate both fabrication speed and track durability:
- Why Commercially Pure Grade 1 & Grade 2: CP Grade 1 (
UNS R50250 / Werkstoff 3.7025 / ВТ1-00) offers the highest elongation and ductility for tight mandrel bends, slip-joint swaging, and collector flaring without work-hardening cracks. CP Grade 2 (UNS R50400 / Werkstoff 3.7035 / ВТ1-0) provides higher yield strength for straight mid-pipes, muffler canisters, and underbody runs while maintaining smooth, predictable weld pool fluidity during back-purged TIG welding. - The 1.0–1.2 mm (0.039”–0.047”) Wall Sweet Spot: Paper-thin
0.8 mm (0.031")tubing saves weight on drag-spec builds but demands extreme heat control and can fatigue under high-RPM harmonic vibration. Conversely,1.0 mm (0.039")and1.2 mm (0.047")walls provide the ideal structural balance — cutting weight by roughly 45% compared to stainless steel while resisting exhaust gas thermal shock and weld-toe cracking. You can compare exact tube mass per meter or foot using our Weight & Allowance Calculator.
Standard Exhaust Tubing Size Matrix
| Imperial OD | Metric OD | Standard Wall Thicknesses | Available Formats |
|---|---|---|---|
| 1.50” & 1.75” | 38.1 mm & 44.5 mm | 1.0 mm (0.039"), 1.2 mm (0.047") | Straight lengths, mandrel bends, laser pie cuts |
| 2.00” & 2.50” | 50.8 mm & 63.5 mm | 1.0 mm (0.039"), 1.2 mm (0.047") | Straight lengths, mandrel bends, laser pie cuts |
| 3.00” | 76.2 mm | 1.0 mm (0.039"), 1.2 mm (0.047") | Straight lengths, mandrel bends, laser pie cuts |
| 3.50” & 4.00” | 88.9 mm & 101.6 mm | 1.0 mm (0.039"), 1.2 mm (0.047"), 0.8 mm (0.031") | Straight lengths, laser pie cuts, merge cones |
Ultrasonically Cleaned & Individually Sealed Pie Cuts
Any fabricator who has built a complex twin-turbo titanium exhaust knows that bandsaw-cutting, belt-sanding, deburring, and acetone-wiping 200 individual pie-cut rings takes longer than welding the exhaust itself. Residual hydrocarbon oils or microscopic burrs left inside the tube cause instant porosity, gray oxide contamination, and embrittlement in a titanium TIG weld.
Through our partner network’s multi-axis rotary Titanium Laser Cutting lines, every pie cut and coped tube joint follows a strict four-stage weld-prep protocol:
- High-Purity Argon Rotary Laser Cutting: Multi-axis fiber lasers cut
4.5°,9°, and15°miter segments with zero mechanical clamping distortion or ovality, shielded by high-purity argon so the cut face remains bright and free of alpha case. - Inner & Outer Edge Deburring: Both ID and OD edges are mechanically dressed so segments sit flush with zero gap during tacking and autogenous fusion welding.
- Ultrasonic Degreasing Bath: All segments are ultrasonically cleaned in multi-stage baths to strip away any trace of mill lubricants, handling oils, and particulates.
- Individually Sealed Packaging: Dried segments are sealed in individual protective bags by size and angle. Welders can tear open a pack at the bench, fixture the rings on the purge mandrel, and weld immediately out of the bag.
Matching CNC-Machined Exhaust Hardware
To keep your entire fabrication BOM under one traceable heat-lot package, we supply matching components produced via Titanium CNC Machining:
- CNC-Turned V-Band Flanges: Male/female interlocking V-band rings in Grade 2 (
UNS R50400 / 3.7035 / ВТ1-0) and Grade 5 (Ti-6Al-4V / UNS R56400 / Werkstoff 3.7165 / ВТ6) matched to2.0" (50.8 mm)through4.0" (101.6 mm)tubing. - O2 Sensor Bungs (
M18×1.5): Stepped and saddle-radiused wideband lambda bosses in CP Grade 2 for distortion-free fillet welding. - Laser-Cut 2-Bolt / 3-Bolt Flanges & Head Flanges: Cut from
8.0–12.7 mm (0.315"–0.500")plate per your CAD/DXF port geometry. - Solid Titanium Exhaust Hanger Rods:
Ø 8.0 mm (0.315"),Ø 9.5 mm (0.375"), andØ 12.7 mm (0.500")Grade 2 rod with formed barb ends.
Quality Documentation & Ordering
Every shipment includes a Material Test Certificate (MTC) with heat-lot traceability and Certificate of Conformance (CofC) verifying chemical composition (including low interstitial O, N, C, H levels critical for weld ductility) and mechanical properties. Dimensional tolerances and delivery schedules are confirmed per drawing and order specification.
Request a Quote for This Product
Send your drawing or specification and we will reply within 24 hours.
Quick Contact
Quality Assurance
- ✓ Material Test Certificate (MTC) with Every Order
- ✓ ASTM / ASME / AMS Standard Compliance
- ✓ Third-party Inspection Available
Related Products
-
Titanium Tubes
Titanium Tubes