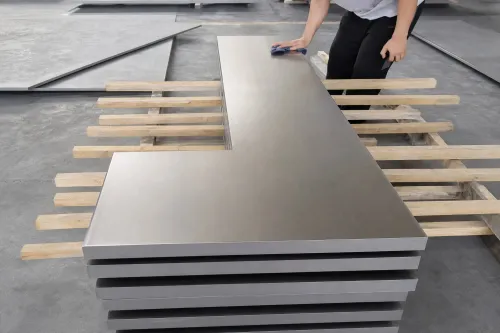
Stop Wasting Carbide Cutters on Mill Scale and Alpha Case
When CNC Machine Shops and custom Knife Making & Custom EDC studios buy raw hot-rolled black-skin titanium plate, the first machining operation is always the most expensive. Raw mill plate carries an oxygen-enriched surface layer (alpha case), abrasive mill scale, and rolling thickness variations. Skimming that crust in your own CNC vertical machining center rapidly chips expensive AlTiN-coated carbide end mills, consumes spindle hours on low-margin stock preparation, and releases asymmetrical residual stresses that cause thin plates to bow or warp once unclamped.
Through our certified partner facilities, we supply vise-ready, pre-machined titanium blanks and double-side surface-ground sheets. By shifting rough scale removal, stress-balanced grinding, and datum squaring upstream, your shop receives clean, bright titanium stock that goes straight into soft jaws, vacuum chucks, or 5-axis tombstones.
Two Core Pre-Machined Delivery Formats
Depending on your finished part thickness and fixturing method, we supply pre-finished flat stock in two distinct configurations. Target thickness tolerances, flatness, and parallelism are evaluated per drawing, feature geometry, and batch quantity and locked in your order confirmation.
| Feature / Specification | 6-Side Milled & Squared Plate Blanks | Double-Side Surface-Ground Sheet & Thin Plate |
|---|---|---|
| Thickness Range | 6.35–76.2 mm (0.250"–3.000") | 1.0–12.7 mm (0.040"–0.500")Includes popular knife & instrument gauges: 1.6 mm (0.063"), 2.0 mm (0.080"), 2.5 mm (0.100"), 3.18 mm (0.125"), 3.56 mm (0.140"), 4.06 mm (0.160") |
| Primary Process | Precision face milling on top/bottom faces + edge squaring on all 4 perimeter sides | Symmetrical multi-pass cold wet surface grinding on both flat faces |
| Surface Condition | 100% free of mill scale and alpha case; clean machined datum surfaces | Bright, uniform ground finish ready for CNC profiling, stonewashing, or anodizing |
| Dimensional & Datum Control | Orthogonal edges and parallel faces evaluated per drawing & batch quantity | Uniform gauge thickness and stress-balanced flatness evaluated per drawing & batch quantity |
| Primary Applications | 5-axis structural brackets, marine manifolds, ROV end caps, multi-part CNC fixture plates | Folding knife scales, integral frame-lock bars, backspacers, precision instrument baseplates |
Grades & Multi-Standard Specifications
We prepare milled and surface-ground blanks across the three primary workhorse titanium grades, supplied with a Material Test Certificate (MTC) with heat-lot traceability and Certificate of Conformance (CofC):
- Grade 5 (
Ti-6Al-4V|UNS R56400|Werkstoff 3.7165|ВТ6): The benchmark alpha-beta alloy for high-strength CNC structural components, motorsport brackets, and spring-temper folding knife frame locks. - Grade 23 (
Ti-6Al-4V ELI|UNS R56407|Werkstoff 3.7165-ELI|ВТ6С): Extra-Low Interstitial variant offering superior fracture toughness and cryogenic/subsea reliability for precision housings and high-end custom hardware. - Grade 2 (
Commercially Pure Titanium|UNS R50400|Werkstoff 3.7035|ВТ1-0): Optimal corrosion resistance and formability for marine fluid plates, chemical manifolds, and decorative inlaid scales.
Critical Engineering Controls for Precision Blanks
Ordering ground or milled titanium stock requires more than just calling out a nominal thickness. Through our partner network, we enforce three workshop-focused controls:
1. Symmetrical Wet Grinding to Prevent Thin-Sheet Warping
Titanium’s low thermal conductivity traps grinding heat at the surface. If a thin sheet (1.0–4.06 mm / 0.040"–0.160") is ground aggressively on one side, localized thermal expansion and uneven residual stress removal will cause the sheet to curl like a spring. Our certified partner facilities use flood-cooled, low-infeed symmetrical grinding passes, alternating between top and bottom faces to balance internal stresses and deliver dead-flat stock for vacuum fixtures and fine-feature pocketing.
2. Rolling Grain Direction Marked on Every Blank
Rolled titanium sheet and plate exhibit directional grain structure. For Knife Making & Custom EDC manufacturers cutting integral lockbars, or machine shops milling thin cantilevered flexures, cutting across versus along the grain changes both the effective elastic modulus and flexural fatigue life. On request, we laser-mark or stencil the primary rolling grain direction on every blank so you can nest your CAM toolpaths with consistent orientation.
3. Single Heat Lot Traceability
When running a production batch of 50 to 500 CNC parts, mixing titanium sheets from different ingot melts leads to unpredictable springback during thin-wall finishing and visible color shifts during Type III voltage anodizing. We support Single Heat Lot fulfillment, ensuring every blank in your release originates from the same master melt lot.
4. Near-Net Waterjet Profiling + Surface Grinding
Instead of buying full rectangular sheets and milling away 60% of the metal as chips, combine surface grinding with cold Water Jet Cutting. We can waterjet near-net perimeters (with zero heat-affected zone) and surface-grind the top and bottom faces to final thickness—delivering stackable part blanks with a 1.0–2.0 mm (0.040"–0.080") peripheral machining allowance.
Estimate Blank Weight & Machining Allowance
Before submitting your drawing, you can calculate the exact theoretical weight of your finished blank—including custom milling allowances and kerf loss—using our interactive Weight & Allowance Calculator. Switch to Machining Allowance Mode to compare raw plate weight against pre-squared net blank weight.