When purchasing titanium bars for precision CNC machining, aerospace structural components, or medical implants, procurement teams frequently encounter significant quote spreads for the exact same alloy grade, such as Grade 5 (Ti-6Al-4V) or Grade 2 commercially pure titanium. The cost variance is substantial. A primary driver behind this pricing hierarchy is the bar mill surface condition and sizing refinement: Centerless-Ground, Lathe-Peeled (Turned), and Black Hot-Rolled.
Actual manufacturing and fulfillment data confirm a clear pricing gradient: centerless-ground polished bar > lathe-turned peeled bar > black-surface hot-worked bar, with delivery lead times typically ranging from 5 to 30 days depending on order tonnage. The lead-time window varies. However, making procurement decisions solely on raw per-kilogram purchase price frequently lures machine shops into an expensive total-cost trap marked by excessive tool wear, high scrap rates, and lost spindle hours. This is a common error. This technical guide contrasts the physical tolerances, surface metallurgy, and true finished component economics across all three product forms.
Dimensional Tolerance, Surface Finish, and Process Positioning
Titanium exhibits intense chemical affinity for oxygen, nitrogen, and hydrogen at elevated hot-working temperatures. Rolling at high temperatures naturally generates a dense, hard, and brittle alpha-case layer together with mill scale. Tolerances cannot be blurred. Different surface finishing operations define the achievable dimensional tolerance classes and determine the downstream manufacturing envelope.
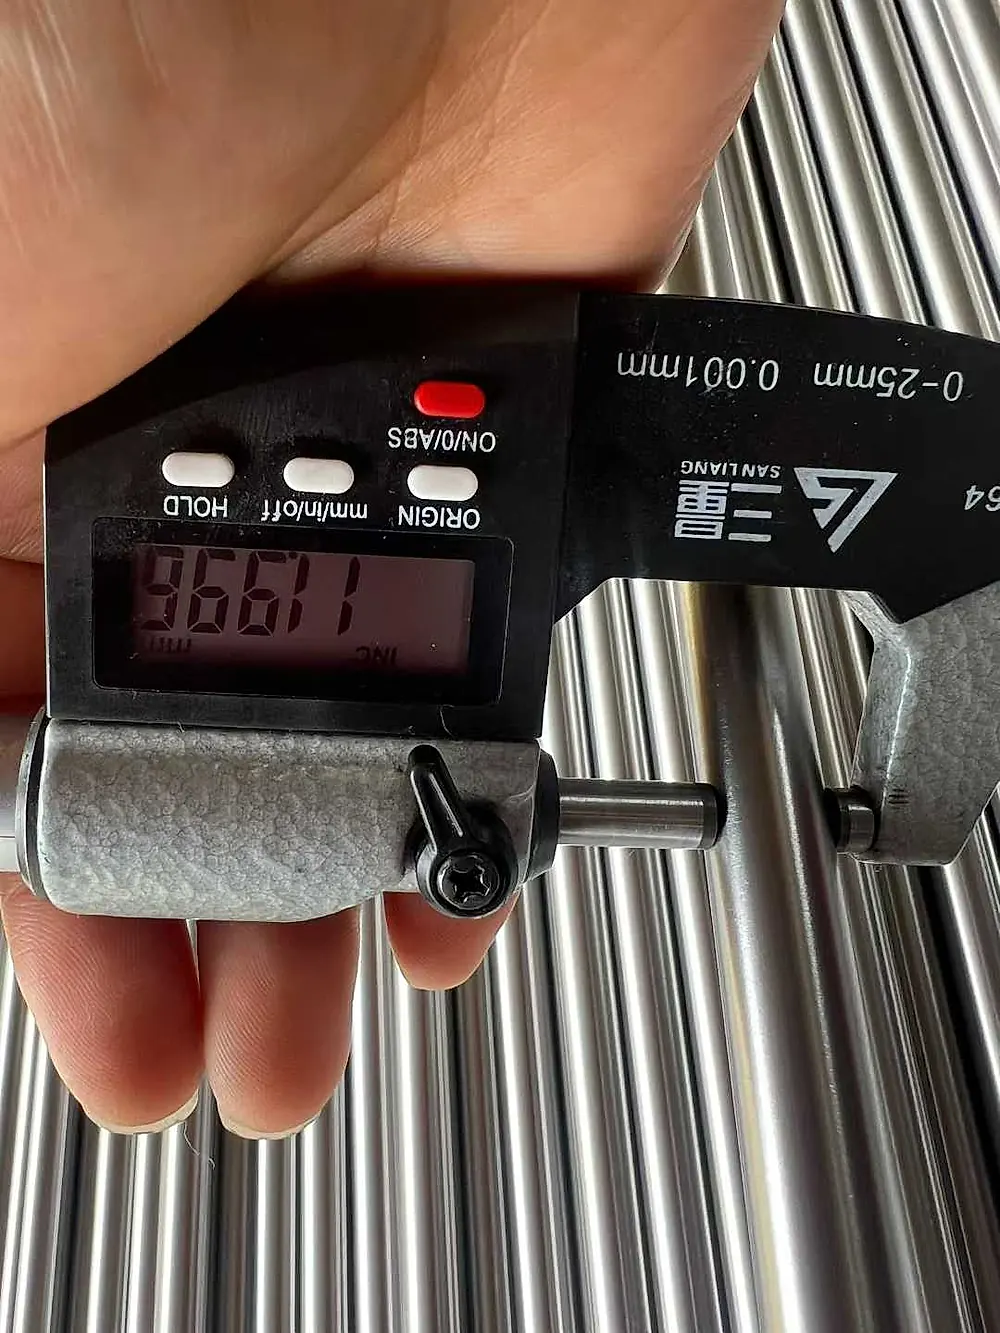 Figure 1: Quality control inspector verifying diameter tolerance and ovality on ultrasonically cleaned ground titanium bars, ensuring consistent h7 compliance across the entire batch.
1. Centerless-Ground Bars
- Dimensional Tolerance and Ovality: Typically manufactured to ISO h7 or high-precision h6 tolerances. For diameters between 10 mm and 25 mm, the diameter tolerance spans +0/-0.015 mm to +0/-0.009 mm, with cylindrical ovality held within half the tolerance bandwidth.
- Surface Roughness: Ra 0.4 μm to 0.8 μm, displaying a clean, uniform, mirror-like metallic luster.
- Straightness Control: Certified partner facilities processing medical implant Ti-6Al-4V ELI (Grade 23) and aerospace ground bars utilize multi-pass centerless grinding coupled with precision roll-straighteners to guarantee straightness within ≤ 0.3 mm/m.
- Primary Applications: Engineered specifically for Swiss-type automatic CNC sliding-headstock lathes, dental implant abutments, orthopedic bone screws, aerospace hydraulic connectors, and precision sensor probe housings.
2. Lathe-Peeled / Turned Bars
- Dimensional Tolerance and Ovality: Conforms to ISO h9 through h11 tolerance classes. Diameter tolerance bands typically sit between +0/-0.036 mm and +0/-0.100 mm.
- Surface Roughness: Ra 1.6 μm to 3.2 μm, showing fine, regular circumferential turning tool witness marks.
- Surface Peeling Mechanism: Heavy-duty rotary peeling machines cut away 0.5 mm to 1.5 mm per side from hot-rolled or forged stock, entirely removing high-temperature mill scale and brittle alpha-case layers down to sound virgin metal.
- Primary Applications: General 3-axis and 5-axis CNC machining, structural shafts, flanges, valve stems, and feed stock for cold-heading or warm-heading bolt blanks.
3. Black Hot-Rolled Bars
- Dimensional Tolerance and Ovality: Modern continuous rolling mills—equipped with 18 high-speed rolling stands and 14 micro-tension sizing stands—hold hot-rolled titanium bar roundness and diameter tolerances tightly within ≤ 0.15 mm. In contrast, conventional open mills exhibit wider fluctuations of ± 0.5 mm to ± 1.5 mm.
- Surface Condition: Encased in dark oxide scale with a brittle, oxygen-enriched alpha-case layer extending 0.1 mm to 0.3 mm deep into the substrate.
- Primary Applications: Secondary open-die forging, seamless ring rolling blanks, and closed-die drop forging. Never suitable for direct high-speed CNC machining or cyclic fatigue service.
Technical Specification and Procurement Comparison Matrix
To assist engineering and procurement teams in structuring unambiguous RFQs, the matrix below details tolerance bands, testing baselines, and cost multipliers across the three surface conditions: The numbers provide clarity.
| Delivery Condition | Relevant Standards | Diameter Tolerance (ISO) | Surface Roughness (Ra) | Straightness Baseline | Alpha-Case Layer | Relative Material Cost Index | Typical Manufacturing Fit |
|---|---|---|---|---|---|---|---|
| Centerless-Ground | ASTM B348, AMS 4928, ASTM F136 | h6 / h7 (+0/-0.009 to +0/-0.015 mm) | 0.4–0.8 μm | ≤ 0.3 mm/m | Zero (100% sound, clean metal) | Baseline (100%) | Swiss CNC auto-feeders, medical bone screws, aerospace instrumentation |
| Lathe-Peeled | ASTM B348, AMS 4928 | h9 / h11 (+0/-0.036 to +0/-0.100 mm) | 1.6–3.2 μm | ≤ 1.0 mm/m | Completely peeled away | Approx. 86%–90% | Standard 3/5-axis CNC turning and milling, flanges, fasteners |
| Black Hot-Rolled | ASTM B348 | ≤ 0.15 mm (continuous) to ± 1.5 mm | Rough scale | ≤ 2.0 mm/m | 0.1–0.3 mm hard brittle case | Approx. 75%–80% | Secondary hot forging, seamless ring rolling, heavy structural blanks |
The Hidden Total-Cost Calculation: Why In-House Peeling Often Fails
A recurring temptation among machine shops is purchasing black hot-rolled bars because they carry a 15% to 20% discount compared to peeled bars and up to 25% compared to ground stock. Supervisors often assume that since the outer diameter will be turned anyway, doing the rough pass in-house saves money. In reality, accounting for full machine cycles and tool depreciation reveals that this approach is rarely economical. This is a common illusion.
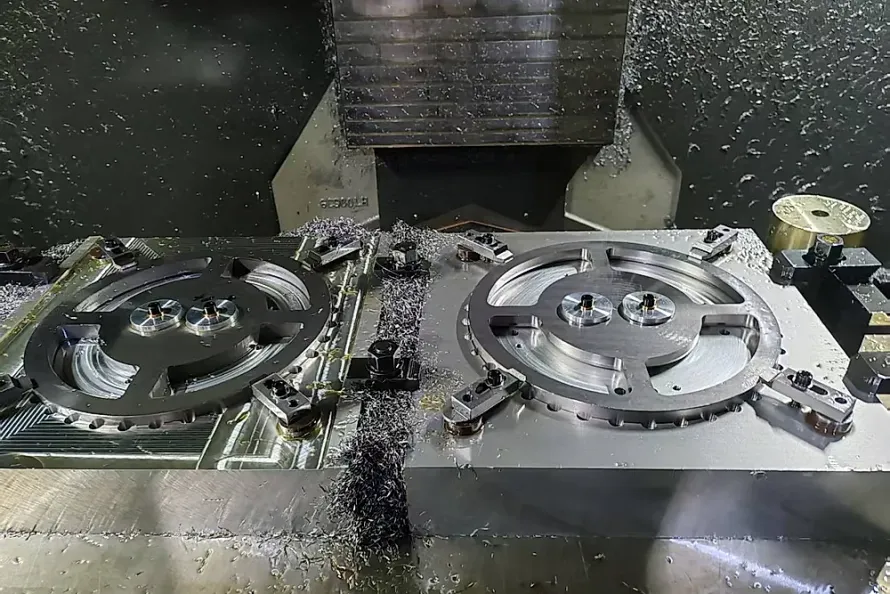
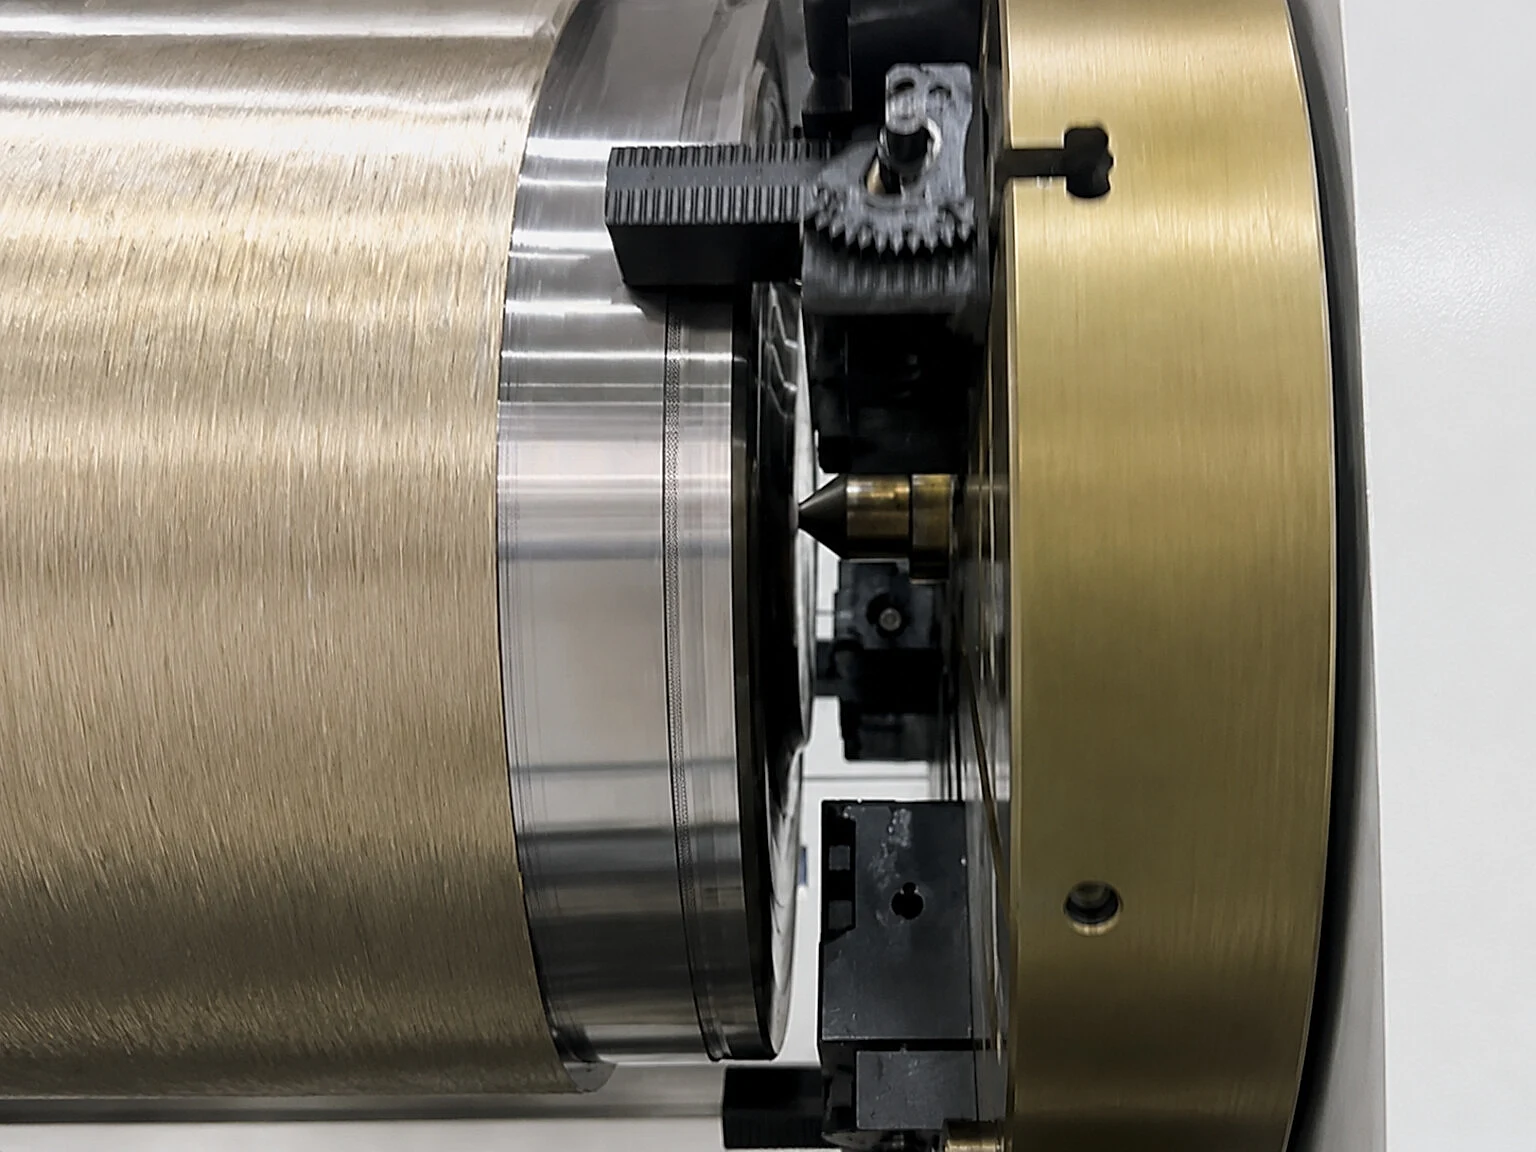 Figure 2: Dedicated heavy-duty peeling lathe cutting through hot-worked titanium stock under flood coolant to remove surface scale without damaging finishing tools.
- Tool Wear and Chipping: Titanium has a low modulus of elasticity (roughly half that of structural steel), causing workpiece spring-back and severe chatter during heavy interrupted cuts. Machining titanium generally consumes 50% more tooling expenditure than carbon steel. The abrasive surface scale and underlying alpha-case reach micro-hardness levels 1.5 times higher than the parent core, causing rapid carbide insert notch wear and thermal cratering. Cutting heat builds quickly.
- Material Scrap and Low Resale Value: Skimming off black scale and correcting roll eccentricity requires an allowance of at least 1.0 mm to 2.0 mm on the radius. On a 30 mm diameter bar, turning down 2 mm on the diameter sacrifices nearly 12% of the bar’s total weight. Loose titanium turnings recover only a small fraction of virgin bar price, representing an unrecoverable material cost loss. Scrap recovery is low.
- Setup Time and Straightness Friction: Black hot-rolled stock typically carries a straightness camber between 1.5 mm/m and 2.5 mm/m. Operators must indicate each raw bar in a 4-jaw chuck and face-center it before taking heavy roughing cuts, consuming valuable spindle hours. In contrast, certified processing platforms run high-throughput rotary peeling lines and multi-roll cross-tension straighteners, producing clean ASTM B348 / AMS 4928 titanium bars at a fraction of a job shop’s internal operational cost.
Swiss CNC Machining Demands on Centerless-Ground Bars
For high-volume miniature components, Swiss-type automatic screw machines deliver unmatched cycle times. Precision standards are stringent. However, their pneumatic bar loaders and carbide guide bushings impose rigid physical tolerances:
- Bushing Clearance Tolerance: A Swiss lathe feeds bar stock continuously through a synchronized guide bushing. If bar diameter varies across an h9 band (a 0.05 mm window), any localized bulge will bind inside the bushing, triggering spindle stalls and potentially crashing live tools. If the bar runs undersized, excessive clearance produces radial deflection under side tool loads, ruining concentricity and surface finish.
- Straightness and Centrifugal Balance: Bar feeder spindles rotate between 6,000 and 10,000 RPM. If straightness deviation exceeds 0.5 mm/m, the spinning bar acts as a centrifugal whip inside the guide channel, generating high-frequency chatter marks on the workpiece and damaging spindle ceramic bearings over time. Certified aerospace ground bars maintain straightness within ≤ 0.3 mm/m to ensure smooth dynamic balance.
- Ultrasonic Cleaning: Centerless-ground bars must be washed in multi-stage ultrasonic solvent tanks to clear residual silicon carbide grinding dust and oil before shipping. Abrasive fines carried into collet assemblies accelerate mechanical wear on expensive CNC spindles. Cleanliness is paramount.
Procurement Verification Checklist for Incoming Quality Audits
When issuing purchase orders and receiving shipments, quality assurance teams should verify these essential technical deliverables: Rigorous verification avoids downtime.
- Material Test Certificate (MTC) Heat Traceability: Must clearly state the melt heat number, vacuum arc remelting (VAR) pass count, interstitial gas chemistry (strictly limiting oxygen, nitrogen, and hydrogen), and room-temperature tensile properties.
- Explicit Surface Delivery Codes: Purchase contracts should designate the exact surface condition code (e.g., “Centerless Ground h7” or “Lathe-Peeled h9”) and explicitly set maximum roughness thresholds (e.g., Ra ≤ 0.8 μm).
- Ultrasonic Inspection Compliance: For Grade 5 (Ti-6Al-4V) bars slated for critical rotating or structural duties, verify ultrasonic testing certificates conforming to AMS 2631 or equivalent NDT standards to confirm zero subsurface voids or density inclusions.
- Protective Packaging Integrity: Ground titanium rods require individual plastic sleeve isolation and solid export wooden crate packaging lined with shock-absorbing foam. Direct metal-to-metal bundling during transport causes superficial scuffing, dinging, or permanent bend deformation. Packaging protects tolerances.
Before releasing formal RFQs, engineering teams can calculate gross-to-net raw material weights using the site’s engineering calculation and unit weight tools; or submit part drawings and tolerance requirements directly to the complimentary drawing review and quotation channel to determine the most cost-effective bar condition and batch manufacturing strategy.